FORMULATING
FUTURE
WITH CHEMICAL EXCELLENCE
Hindustan Silicates & Aluminates (H.S.A) - a leading diversified and integrated chemicals Manufacturer & Supplier with presence across all the streams of Silicates, Aluminates & Allied chemical sources.
Precision-Engineered Formulations for Global Markets
H.S.A represents a benchmark of excellence in sodium silicate and sodium metasilicate manufacturing and chemical processing. Harnessing deep-rooted expertise in silicate manufacturing, we supply robust, high-performance silicates and aluminates engineered to uphold the most rigorous international safety and quality protocols.
HSA - Division
From initial lab concept verification to continuous maritime container dispatching, every batch is scrutinized under strict QC workflows, making H.S.A the preferred partner for complex manufacturing plants worldwide.
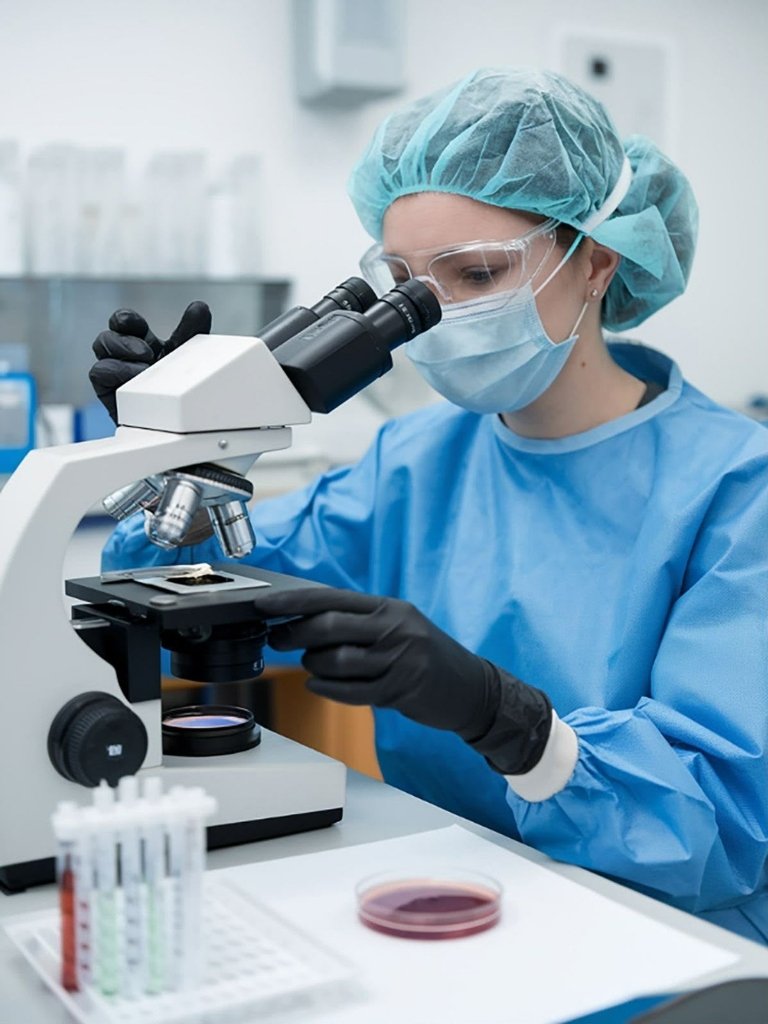
In-House R&D
Continuous analytical synthesis ensuring superior quality, density, grade consistency, and strict moisture control.
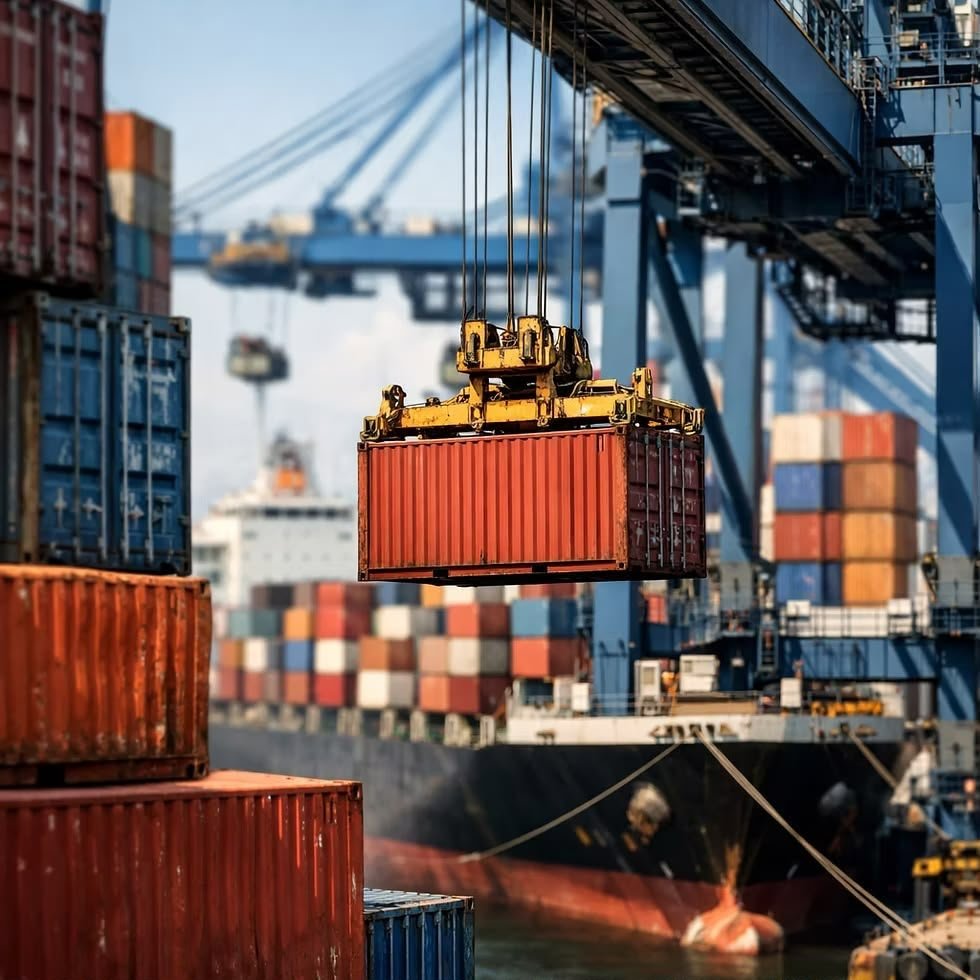
Global Supply Chain
Reliable global logistics with efficient shipping, import, export, and timely industrial deliveries worldwide.
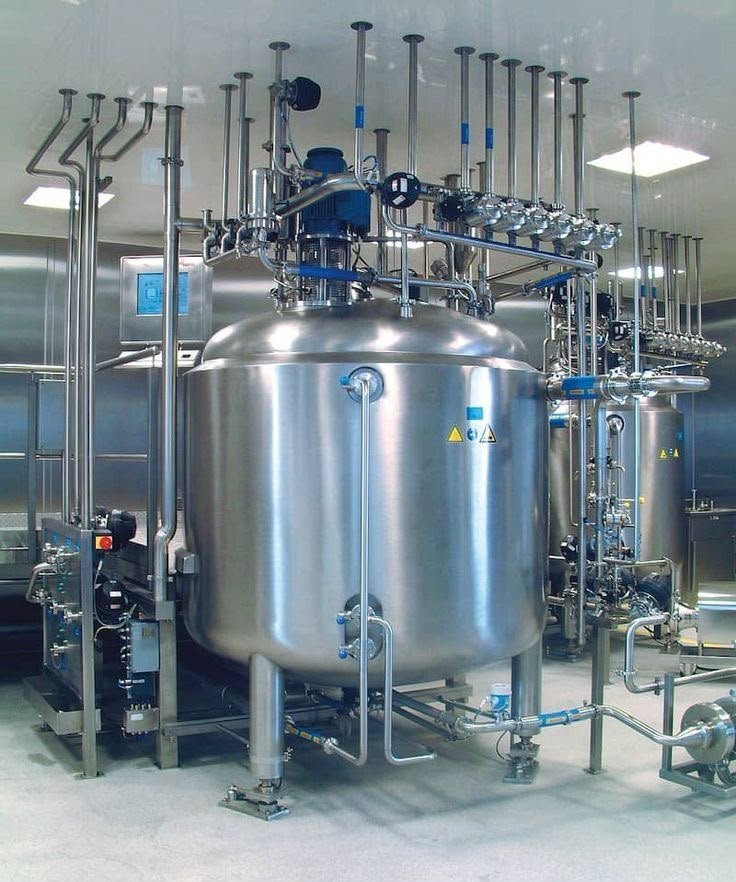
Stockist Network
Extensive warehouse and dealer network ensuring uninterrupted availability of industrial chemicals across India.
Delivering trusted industrial chemical solutions with quality, innovation, and customer satisfaction for over two decades.
Major Industries We Serve Globally
Our precision silicates, aluminates, and minerals act as high-performance solution across diverse industrial workflows.
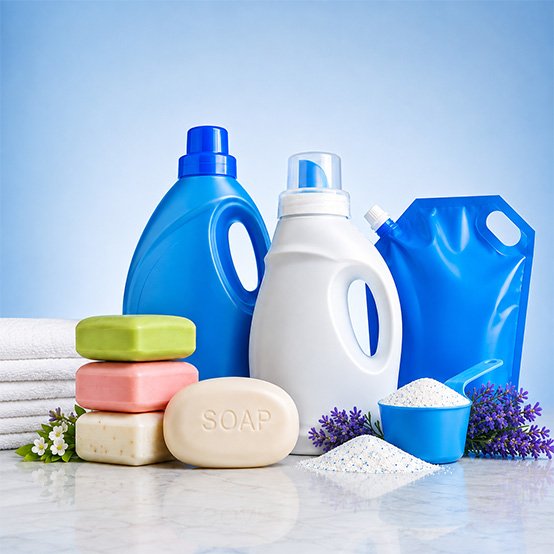
We supply high-grade builders, alkalinity boosters, and anti-redeposition agents that enhance cleaning performance in powdered and liquid detergents. Our solutions optimize emulsification, soften process water, and prevent corrosion in industrial and household washing systems.
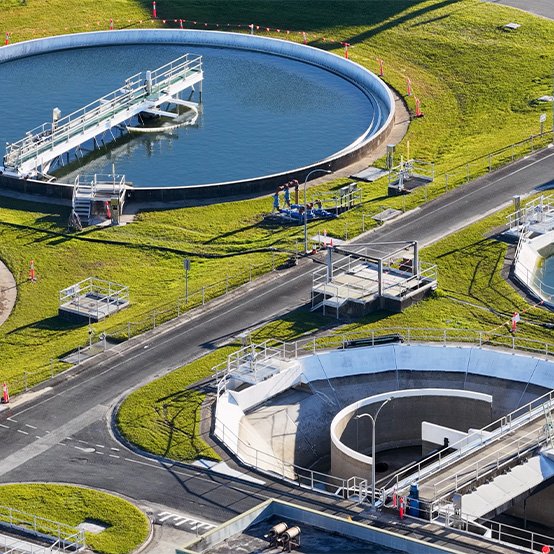
Our chemical formulations act as potent coagulant aids, corrosion inhibitors, and pH stabilizers for municipal and industrial effluent facilities. We help processing plants reduce turbidity, sequester heavy metals, and maintain compliant discharge standards.
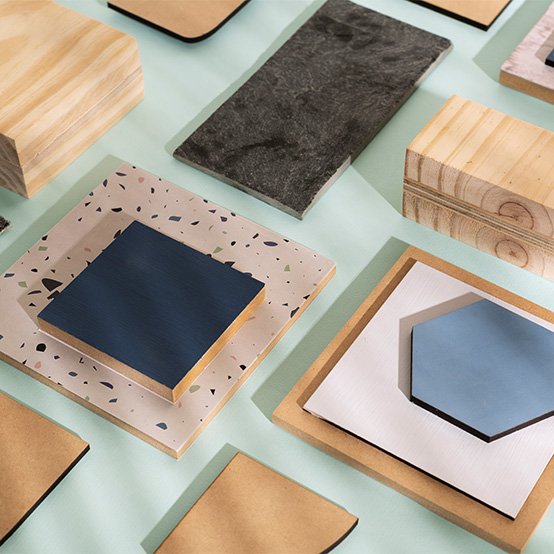
We provide high-efficiency deflocculants and binding additives that optimize clay slip viscosity and improve green strength in ceramic bodies. Our chemical agents ensure uniform casting, defect-free drying, and reduced energy consumption during kiln firing.
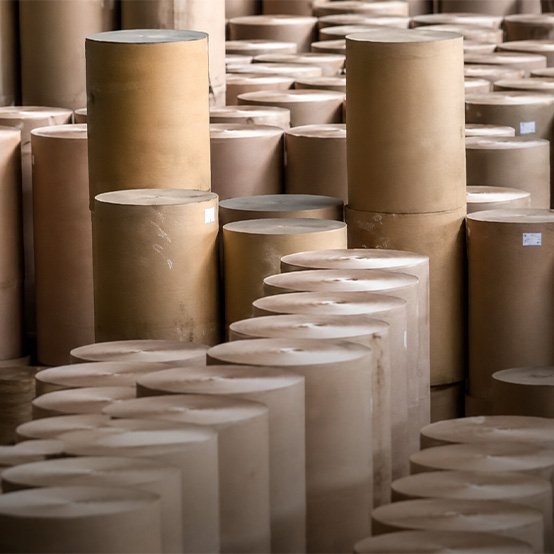
Our functional chemistries enhance de-inking, peroxide bleaching stabilization, and fiber retention throughout the paper manufacturing cycle. We help mills improve sheet brightness, tensile strength, and operational efficiency while minimizing chemical waste.
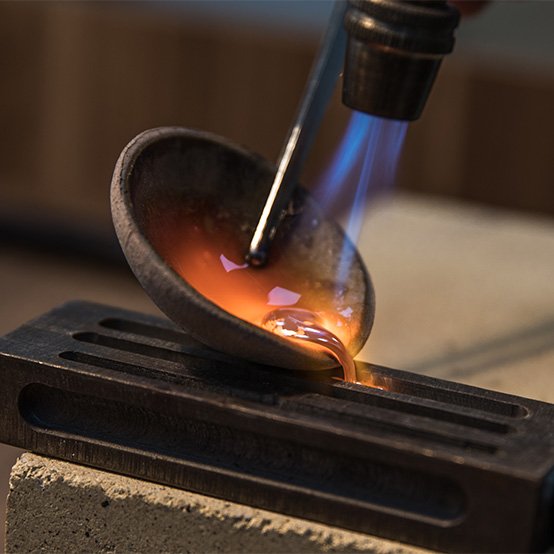
We deliver reliable inorganic binders, core additives, and fast-setting silicate systems engineered for high thermal stability and dimensional precision. Our solutions reduce mold deformation, improve surface finish, and ensure clean shakeout in heavy casting environments.
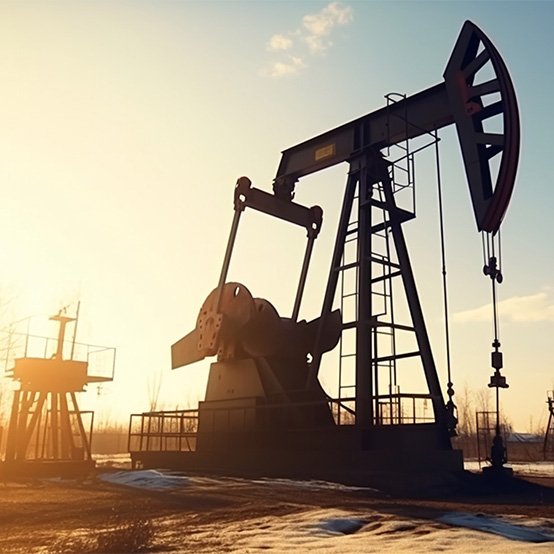
Our drilling mud additives, cementing accelerators, and fluid-loss control agents ensure borehole stability across demanding onshore and offshore wells. We deliver robust chemistries designed to withstand extreme downhole pressures, high temperatures, and corrosive formations.
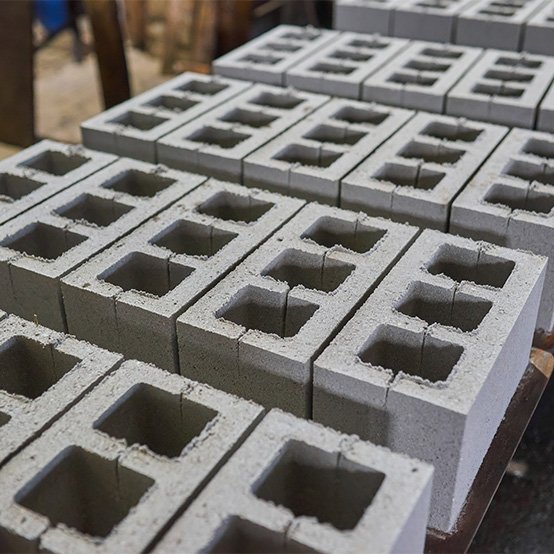
We engineer setting accelerators, surface hardeners, and supplementary binder compounds that accelerate cure rates and boost early compressive strength. Our additives enhance durability, reduce porosity, and mitigate chemical leaching in precast and specialized concrete formulations.
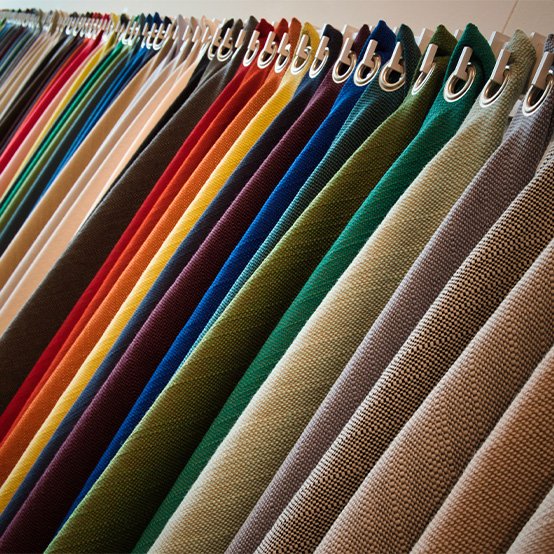
Our specialized processing aids stabilize bleach baths, optimize scouring efficiency, and enhance dye penetration across natural and synthetic fibers. We deliver consistent alkaline buffers that preserve fiber integrity and ensure vibrant, uniform color yields.
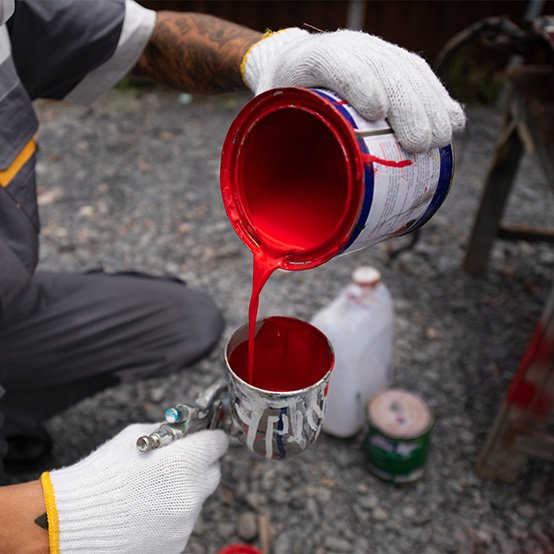
We provide high-purity inorganic binders, pigment dispersants, and mineral extenders that bolster weatherability and film toughness. Our raw materials deliver exceptional scrub resistance, UV stability, and anti-efflorescence performance in architectural and protective coatings.
We provide versatile, high-purity reactive raw materials tailored for downstream synthesis, silica gel production, and catalyst manufacturing. Our consistent quality control guarantees exacting stoichiometry and predictable reaction kinetics for complex chemical processing.
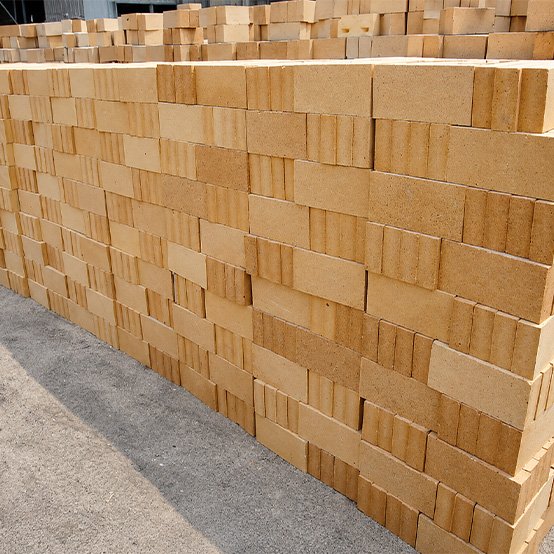
Our heat-resistant binding chemistries and matrix consolidators ensure superior mechanical strength and structural integrity at extreme operating temperatures. They protect refractory linings against thermal shock, slag penetration, and abrasive wear in industrial kilns and furnaces.
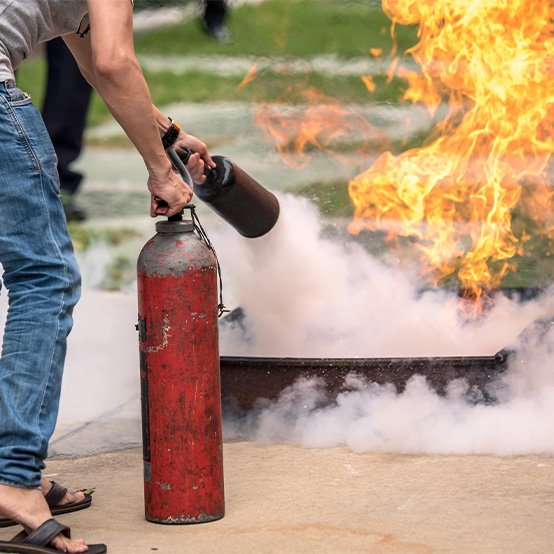
We supply inorganic barrier additives and intumescent precursors that suppress smoke generation and delay flame propagation in polymers, coatings, and textiles. Our eco-friendly chemistries release zero toxic halides while providing dependable thermal insulation.
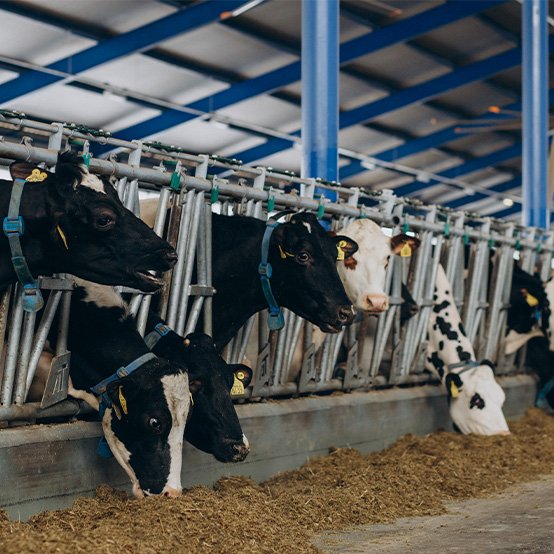
We deliver feed-grade mineral supplements, anti-caking agents, and pellet binders that preserve nutritional integrity and prevent moisture degradation. Our ingredients support gut health, enhance feed flowability, and ensure durable, dust-free pellet formation.
Our certified food-grade processing aids, clarification agents, and anti-caking additives comply with strict global safety and purity regulations. We support high-throughput beverage filtration, nutrient stabilization, and precise pH control in processed food manufacturing.
We supply essential fluxing agents, refining additives, and matrix formers that lower batch melting temperatures and reduce thermal energy demands. Our chemistries guarantee batch homogeneity, bubble-free melt clarity, and enhanced mechanical strength in flat and container glass.
We provide specialized surface-treatment chemicals, flux additives, and protective inhibitors designed for primary smelting and downstream alloy finishing. Our solutions eliminate surface oxidation, improve grain refinement, and prepare aluminium substrates for superior anodizing and coating adhesion.
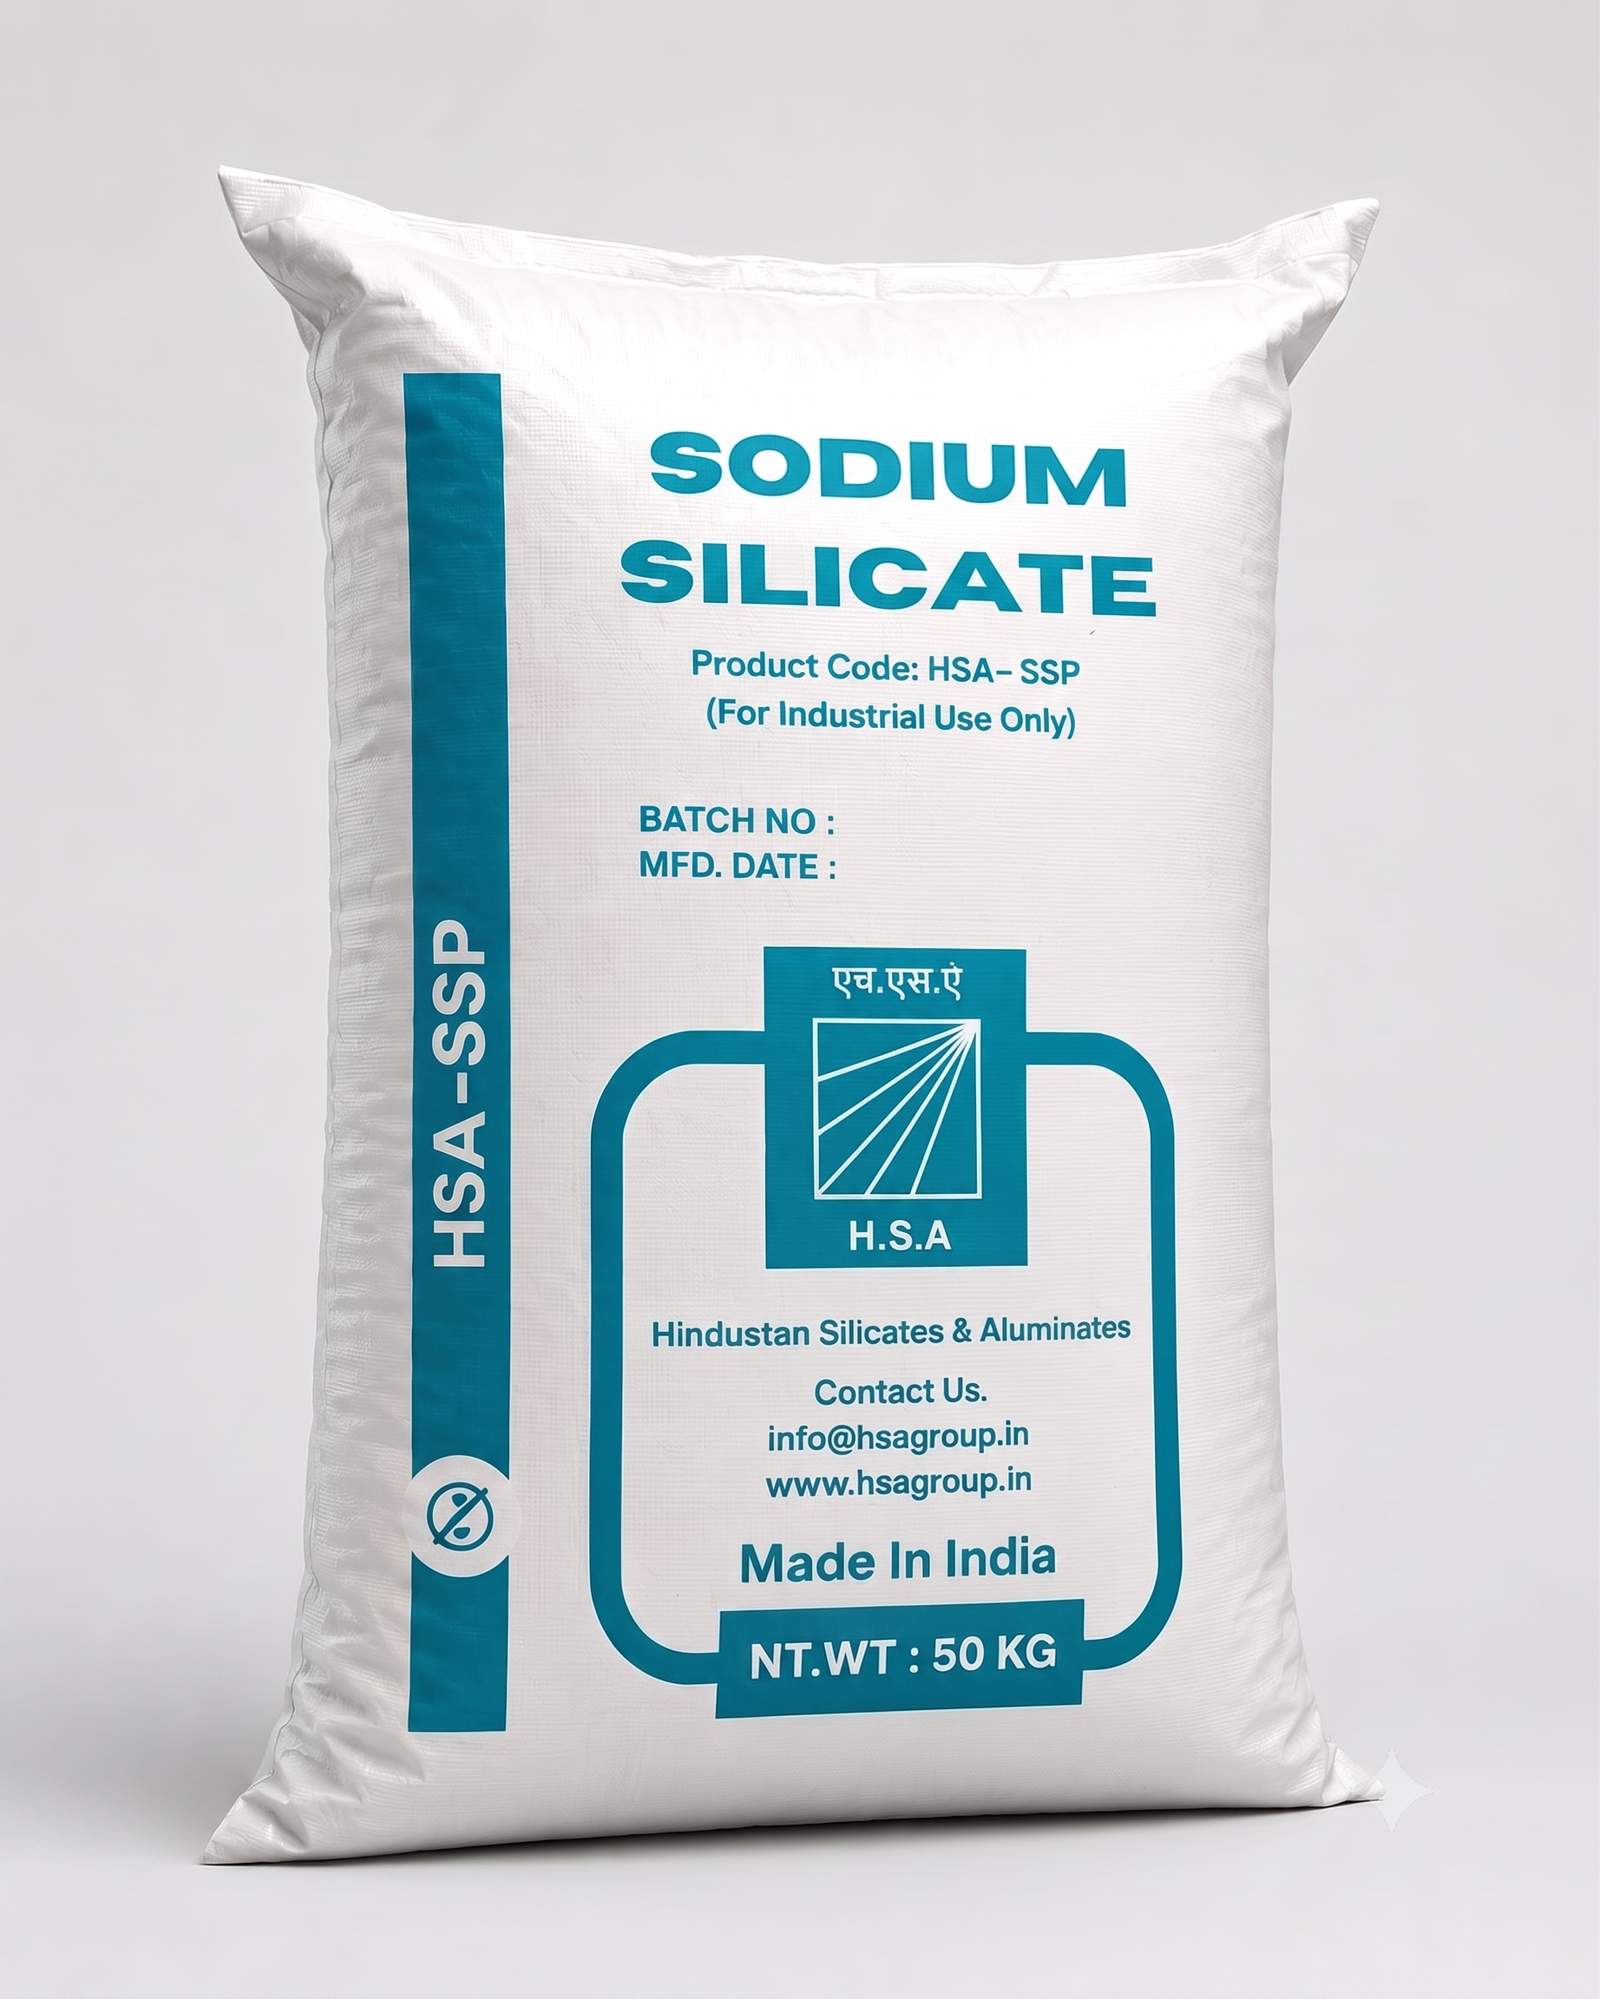
Tough. Anti-Static. Flexible.
Our advanced packaging sets new benchmarks across the industrial chemicals industry, resulting in fully protected, moisture-resistant, and zero-waste deliveries.
Moisture Barrier HDPE Liners
Equipped with highly integrated 100-micron internal liners that seal powders perfectly from tropic dampness or cargo sweat.
Type-B Static Discharge Control
Woven with unique static-control filaments that prevent high voltage build-up, mitigating dust explosion risk during rapid pneumatic silo fillings.
Sea Cargo Certified Strength
Reinforced double chain lock stitches enabling seamless multi-layer stackability on maritime container pallets.
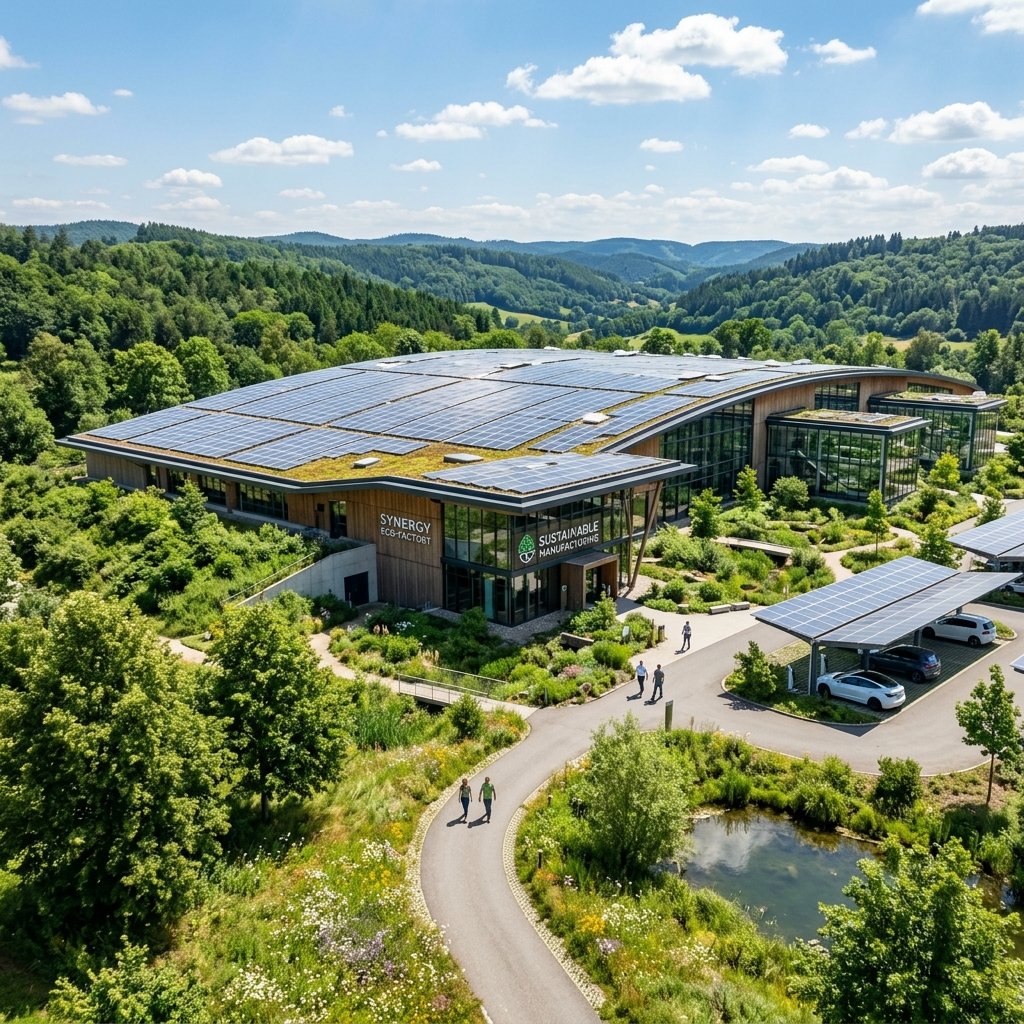
Committed to
Sustainable Growth
Even as we at H.S.A are meeting the demand for 'life-enhancing chemicals', we are doing it responsibly. H.S.A is aspiring and working to not only make a difference to the economy but also the ecology.
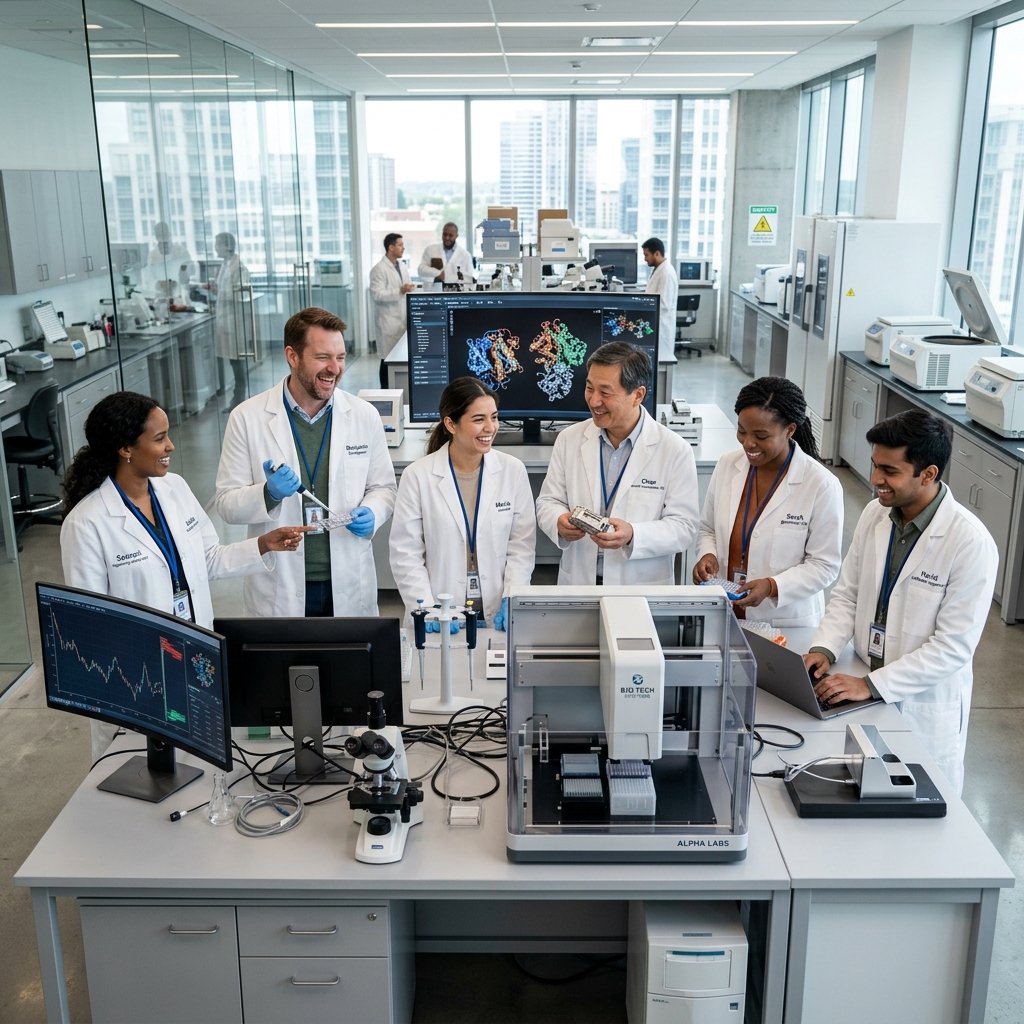
Synergy of
Teamwork in Every Action
At H.S.A, teamwork that is ingrained in our DNA is shaping a new future. This synergy and coherence have shaped the megalith as it stands today, and will shape the world tomorrow.
OUR CORPORATE ECOSYSTEM
ESTEEMED BULK CUSTOMERS & CHANNELS
Grasim
Aditya Birla Chemicals Division
Reliance Industries
RIL Petrochemicals & Polymers
Request For Quotation (RFQ)
Fill in your industrial requirements below. Our commercial procurement team will calculate specific freight logistics rates and respond within 24 business hours.
Request For Quotation (RFQ) Form
Fill in your industrial requirements. Our procurement desk will calculate specific freight logistics rates and respond within 24 business hours.